Introduction
Have you ever paused at the gate of a car plant and wondered what the air inside might be carrying? In many workshops, automotive manufacturing welding fume extraction is the quiet hero — or the silent problem — depending on how it’s done. Recent on-site checks often show elevated particle counts near welding stations (up to several times higher than safe limits), and workers still report irritation, headaches and chronic coughs. So I ask: are we really protecting people and product, or simply ticking boxes?
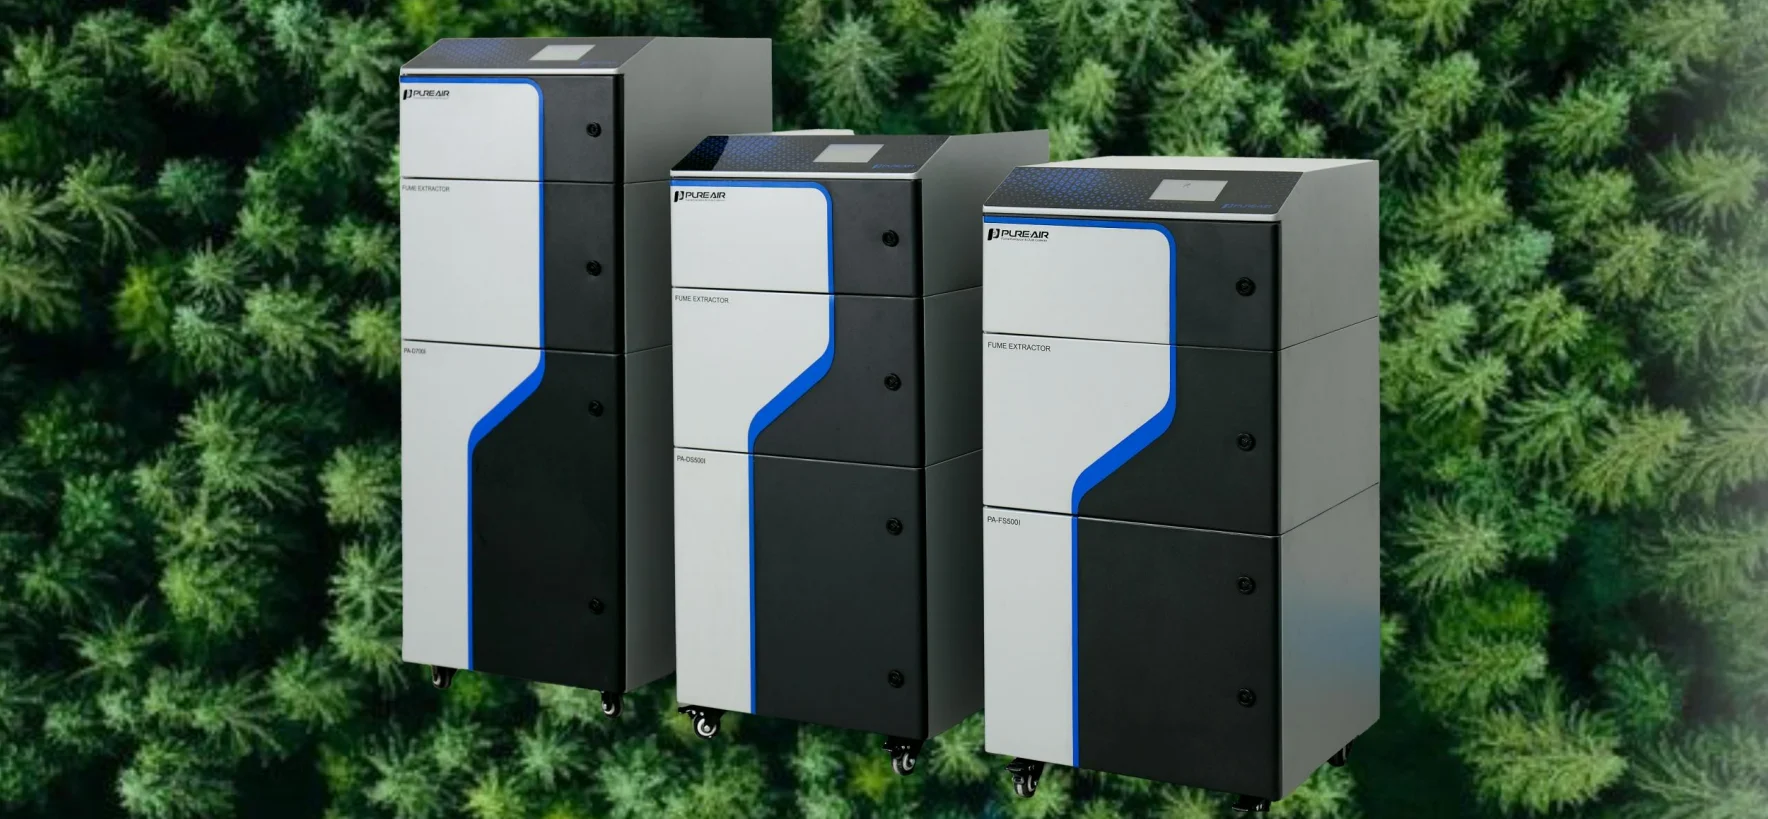
I’ve seen small shops and large assembly lines. The difference often comes down to one thing: how seriously the team treats extraction and filtration. Local exhaust ventilation, source capture arms and ducting matter. But so do training and maintenance. This piece will walk through where the usual fixes fail, what new principles are changing the game, and how you can judge solutions for your plant. Let’s move on to the thorny bits.
Deep Dive: Why Traditional Systems Miss the Mark
When I talk about welding fumes dust collectors, I mean the whole kit — hoods, fans, filters and controls. Many plants buy a unit and assume it will run itself. That assumption costs money and health. In practice, filters clog, airflow drops, and particle counters show a slow creep in duty exposure. HEPA filters help with fine particulates, yes, but without correct airflow balance and routine checks, they do little good. Power converters in older fan drives can falter, leaving suction uneven across bays. Look, it’s simpler than you think: capture at source must be constant, not occasional.
Why do these systems fail?
From my visits I note a handful of repeated faults: poor duct layout that creates back-pressure; mismatched fan curves; inadequate make-up air causing negative pressure in the hall; and weak maintenance regimes. Edge computing nodes and simple sensor networks are underused; teams rarely log trends or predict filter life. As a result, systems either run too hard (wasting energy) or too soft (letting fumes escape). We can fix many of these with modest changes — training, basic data logging, and smarter fan controls. But that requires someone to care and follow through. I care. You should too.
Looking Ahead: New Principles and Practical Metrics
What’s next? New systems blend better capture design with smarter controls. Modern welding fumes dust collectors pair variable-speed drives with simple sensors so suction is tuned to real work rates. Add a particle counter or two and you have meaningful feedback. The principle is clear: monitor, then act. That contrasts with old-school fixed-speed fans and calendar-based filter swaps. I’ve seen plants cut energy use and exposure at the same time — surprising, right? — by tuning rather than over-sizing equipment.
What’s Next?
To evaluate solutions, I use three hard metrics that I ask every supplier about: capture efficiency at the weld (measured), system energy use over a week (logged), and real filter life under your duty cycle. Measure these and you’ll see who knows their stuff. Also consider ease of maintenance and availability of spare parts. Small choices matter: a poorly positioned hood ruins a good collector. We should aim to make systems simple to run, and honest in their performance — no gimmicks. Finally, take a real trial if you can. Short pilots reveal problems fast.
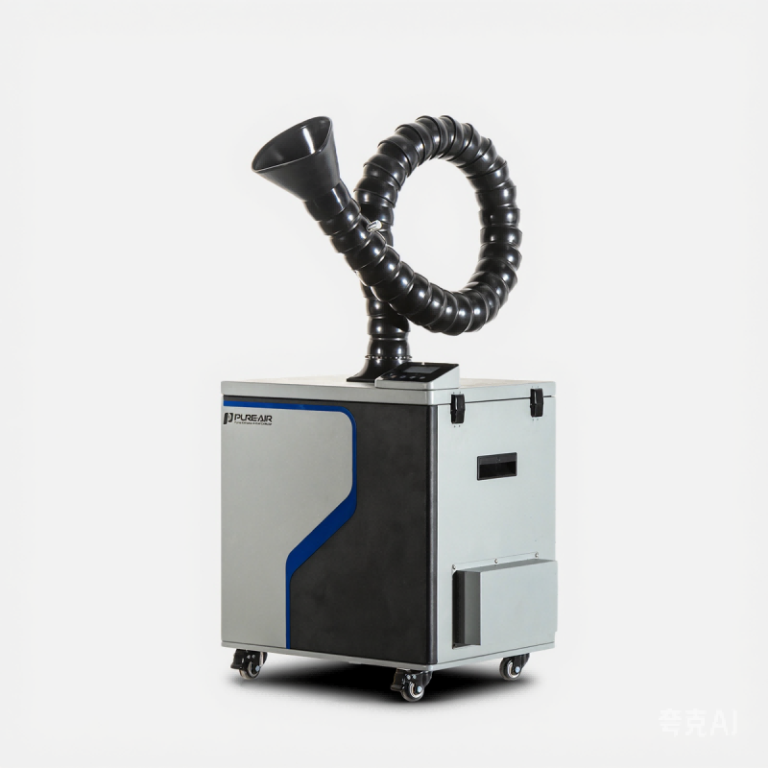
In closing, I’ve learned that better welding fume control starts with questions, not machines. Ask for data, insist on tested capture rates, and plan for upkeep. That’s practical safety. For help and trusted products, consider exploring PURE-AIR — their hands-on approach and clear specs make the choice easier.